Chemical Process Reactor Manufacturers in Nizamabad
- Home
- Chemical Process Reactor
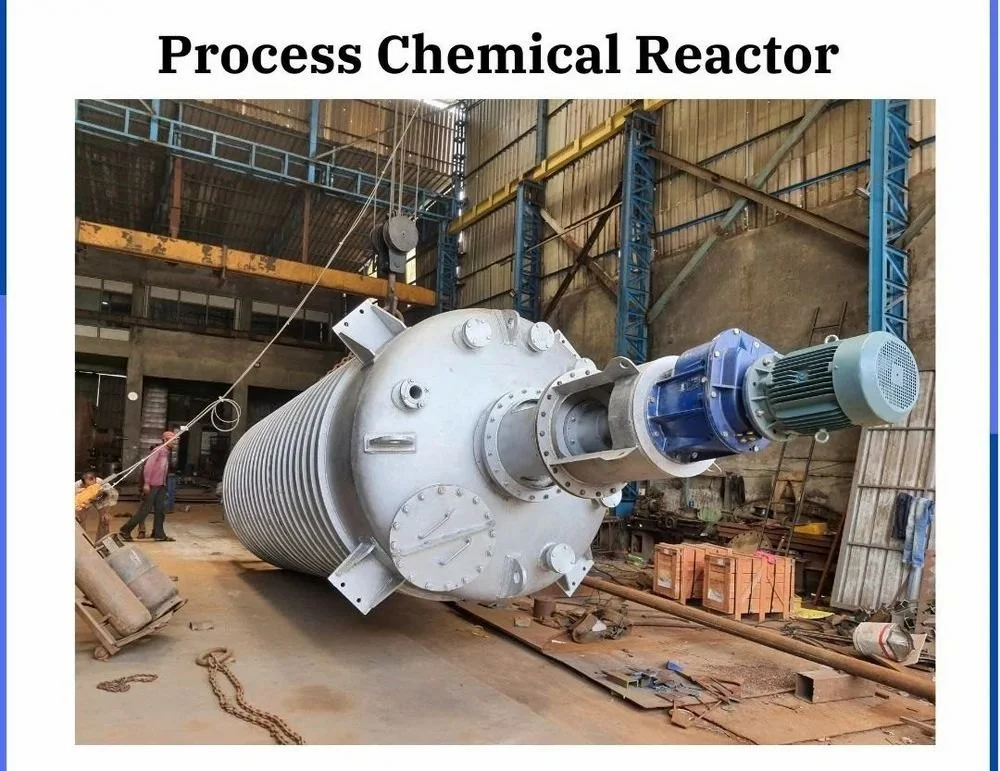
Essentially, the control of temperature, mixing, pressure and compatibility of the components within a chemical batch is the focus of chemical processing. Chemical process reactors aim to provide a controlled environs for the execution of chemical reactions, mixing of reactive components, dissolving, heating, cooling or controlling process parameters.
A chemical process reactor typically comprises a product contact vessel, an agitator, a drive system, and a heating and cooling subsystem. Depending on the application, the vessel can be equipped with a jacket, limpet coil, condenser, vacuum connection, pressure arrangement, temperature sensors, valves, sampling points, and other process accessories.
Agitation is instrumental in ensuring control of product movement and distribution of reactants and heat. The optimum agitator design depends on the characteristics of the material such as density, viscosity, solids content and the nature of the flow.
Chemical Process Reactor Suppliers in Nizamabad
Depending on the prevailing conditions, some reactions may require heating, while others need cooling. Certain formulations may also require vacuum operation, controlled pressure, condensation, or continuous agitation.
As reliable Chemical Process Reactor Suppliers in Nizamabad, we consider the reaction characteristics, batch volume, operating temperature, pressure or vacuum requirements, material viscosity, heat-transfer needs, and agitation requirements before recommending a suitable reactor configuration.
A jacketed reactor can provide indirect heating or cooling through the vessel wall, while a limpet coil arrangement can be used where a different heat-transfer configuration is required. The reactor can also be provided with insulation to reduce heat loss and improve temperature management.
For processes involving volatile components, suitable condenser or vacuum arrangements can be incorporated according to the process requirement. Temperature monitoring and control systems can help operators observe important process conditions during operation.
Product-contact construction is selected according to the nature of the chemicals being processed and the required corrosion resistance. The reactor can be used as a standalone unit or connected with storage vessels, filters, condensers, pumps, and other process equipment.
Chemical Process Reactor Exporters in Nizamabad
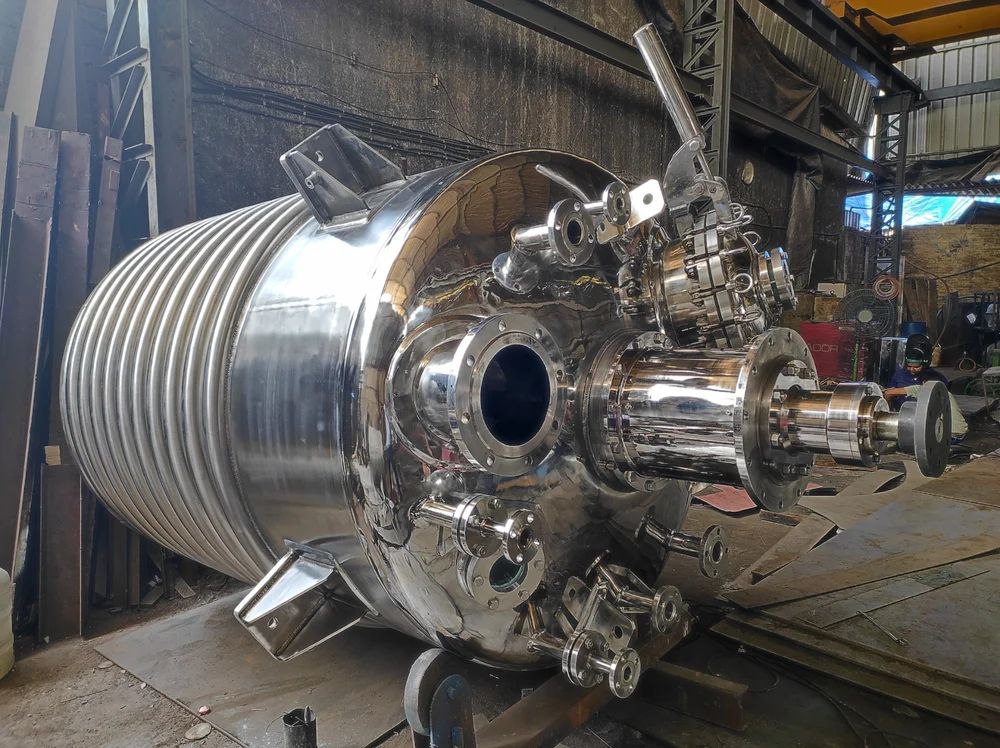
Heat exchangers comprise various sections such as pressure/vacuum components, heating and cooling systems, agitation devices, valves, instruments and supporting structures. Before shipping, appropriate examination and the necessary transport preparations are essential.
As Chemical Process Reactor Exporters in Nizamabad, we provide:
- Pre-Dispatch Inspection: The reactor vessel, agitator, drive system, heating or cooling arrangement, valves, instruments, and major assemblies are inspected before shipment.
- Protective Packaging: Flanges, fittings, instruments, exposed surfaces, drive components, and sensitive assemblies are suitably protected.
- Component Securing: Removable components and delicate equipment are secured to minimize movement during handling and transportation.
- Equipment Documentation: Required equipment and shipment-related documentation can be prepared according to order requirements.
- International Supply: Chemical process reactors can be supplied to pharmaceutical, chemical, cosmetic, herbal, specialty chemical, and allied industries in international markets.
- Dispatch Preparation: Equipment dimensions, weight, lifting points, packing requirements, and transportation conditions are considered before shipment.
Careful export preparation helps protect the reactor and its associated process components during transportation.
Why choose us?
Longstanding Experience: Pharmachem Cosmetics Industries has been manufacturing pharmaceutical and allied processing machinery since 2005. Our experience with reactors, vessels, mixers, dryers, and other process equipment supports the development of equipment for different chemical processing applications.
Application-Based Design: Reactor requirements depend on the chemistry and operating conditions. We consider batch volume, reaction temperature, pressure or vacuum, viscosity, agitation, heat transfer, and material compatibility before developing the equipment.
Controlled Heat Transfer: Jacket or limpet coil arrangements can be incorporated to provide heating or cooling according to the requirements of the chemical process.
Effective Agitation: The agitator is selected according to product viscosity, density, solids content, and required mixing intensity, helping maintain appropriate movement throughout the reaction.
Material Compatibility: Product-contact materials can be selected according to the chemical characteristics of the formulation and the required corrosion resistance.
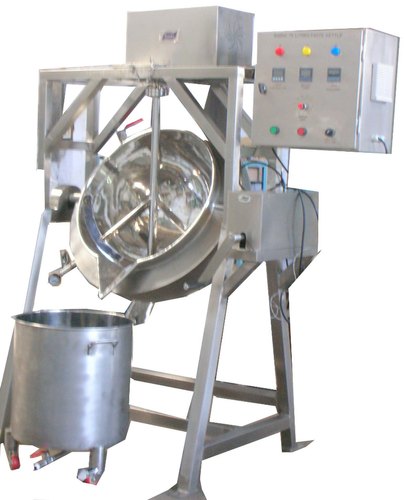
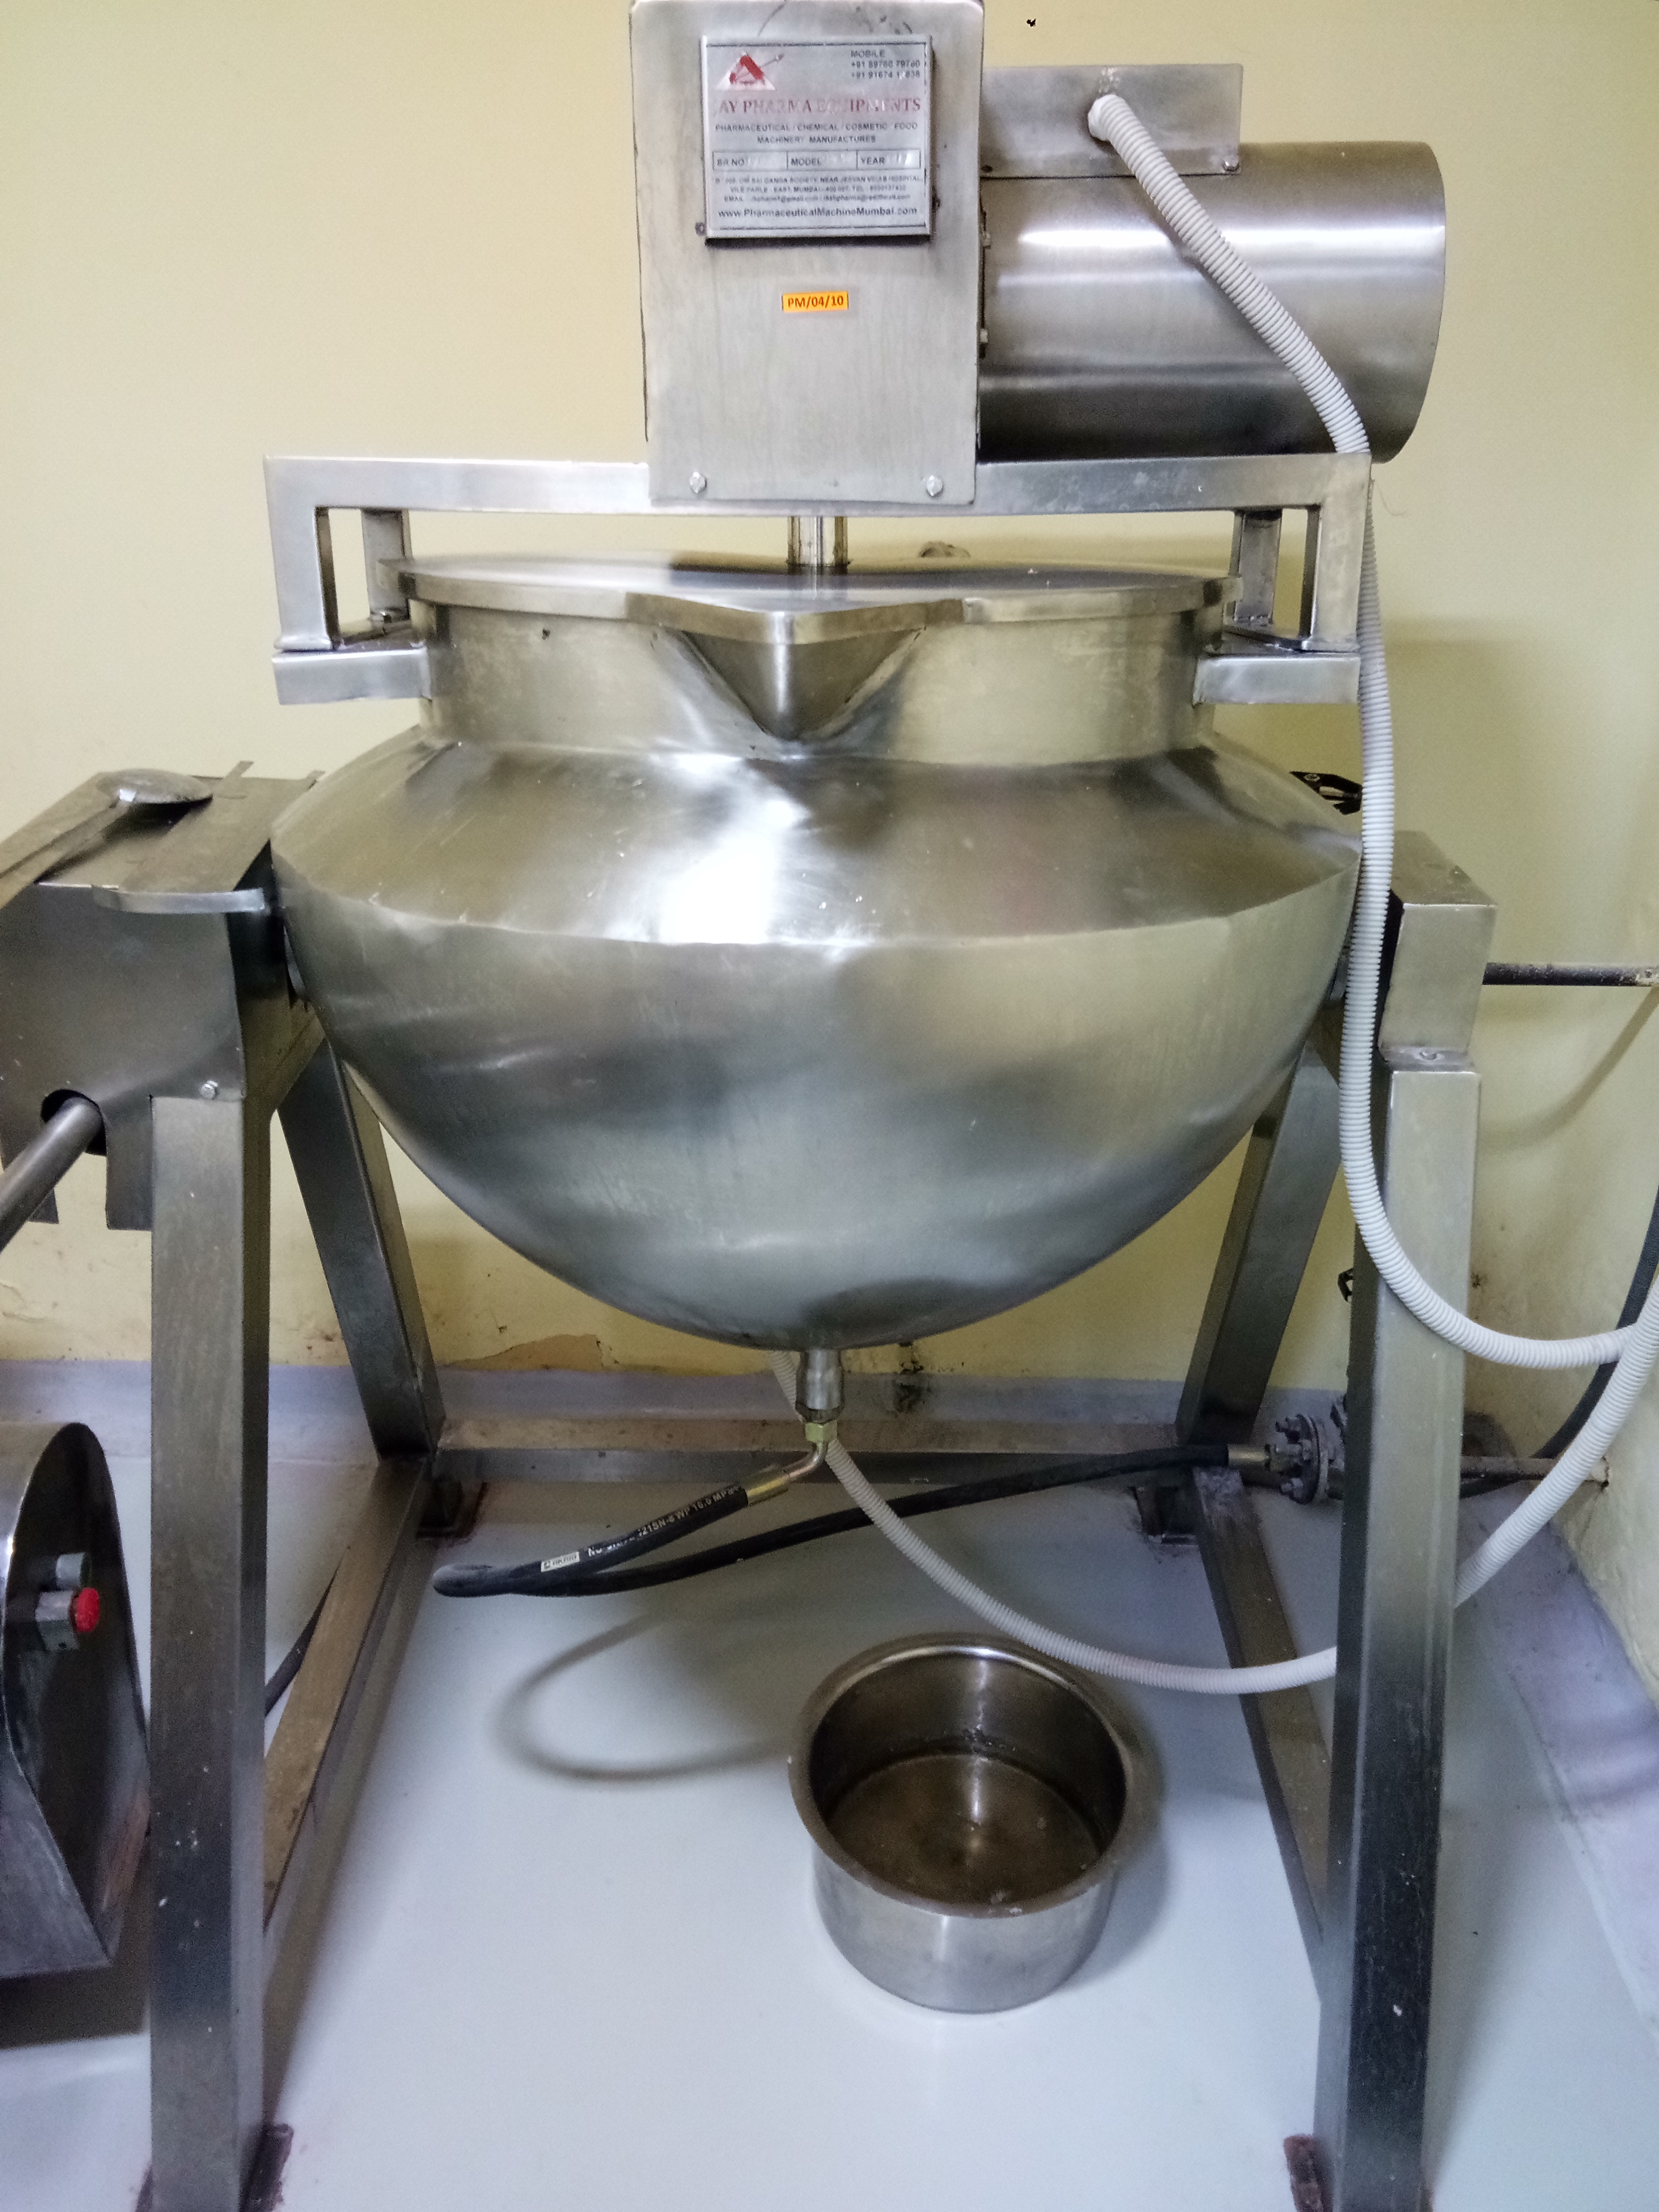
Binder pastes, gel bases, and viscous intermediates all run on one requirement t...
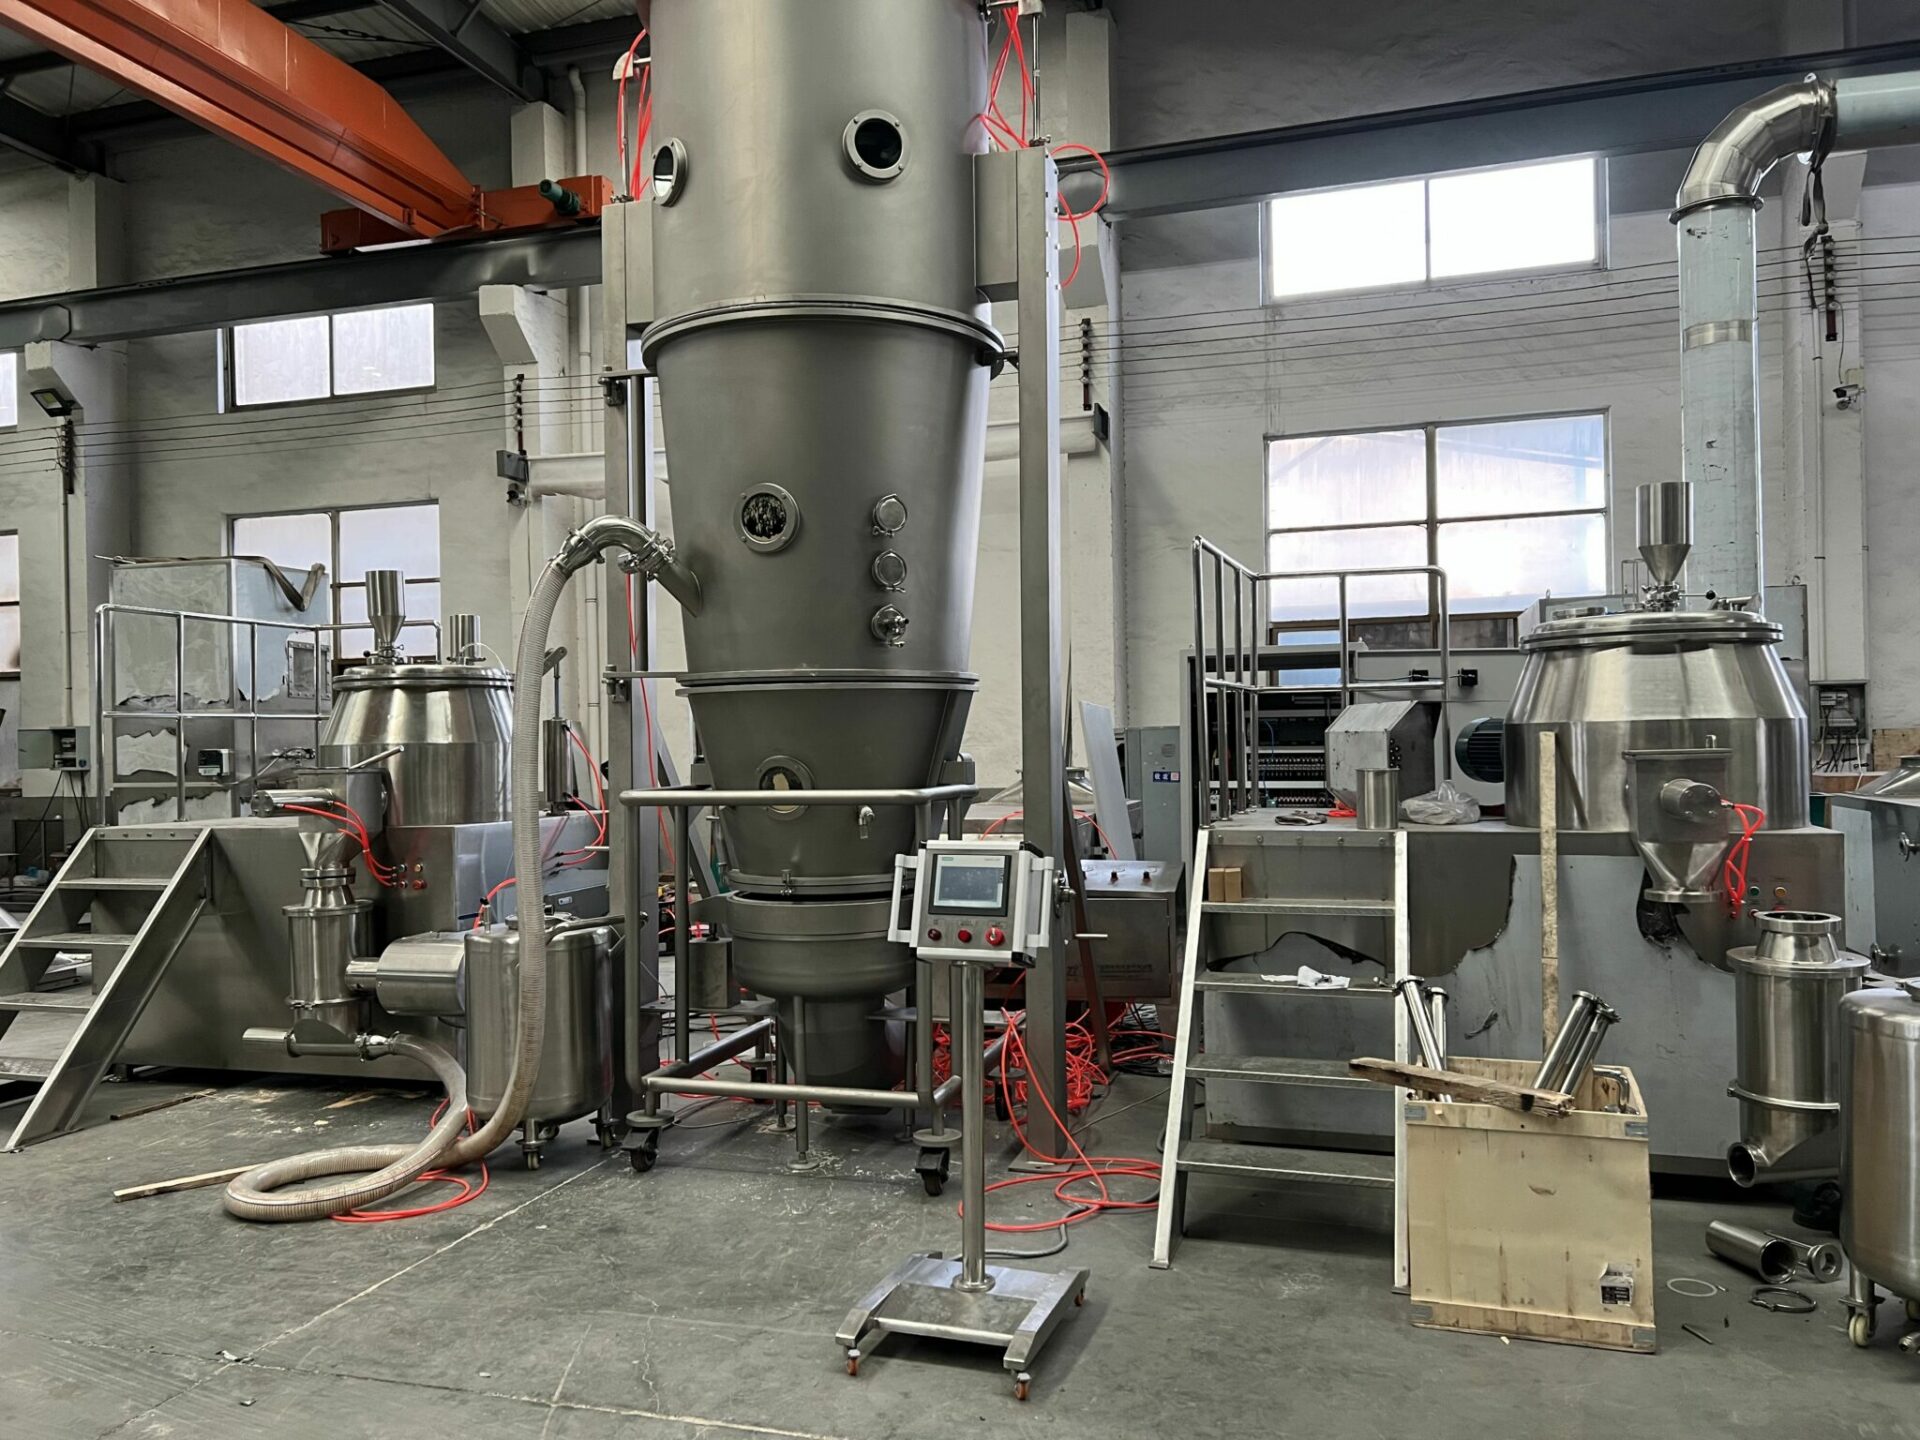
Turning fine powders into free flowing, compressible granules is one of the more...
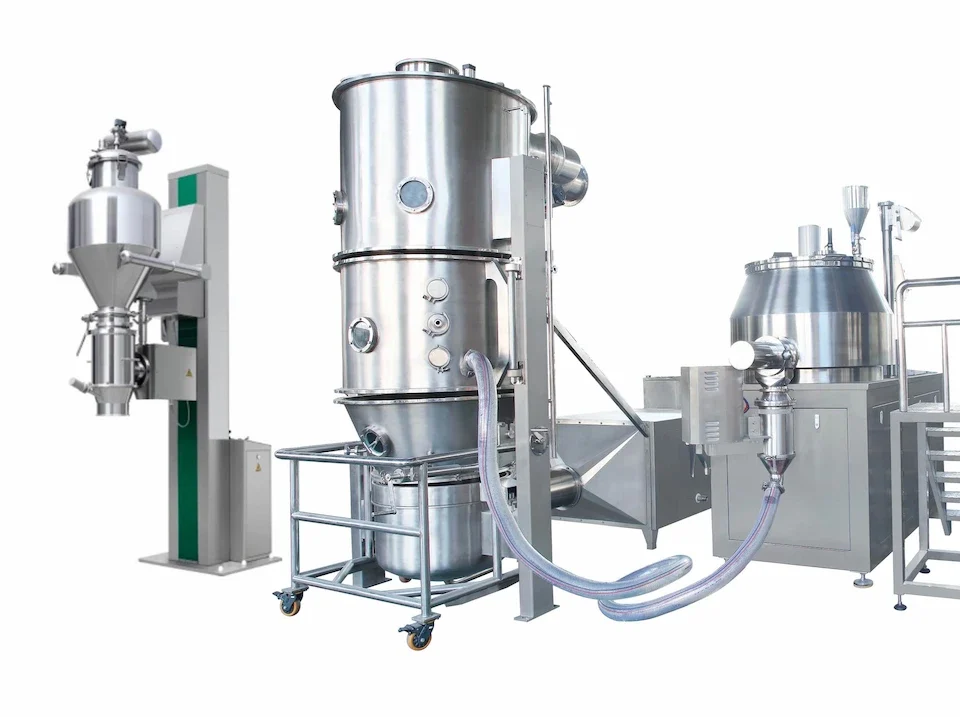
Pharmachem Cosmetics Industries, located in Mumbai Mumbai since 2005, designs an...
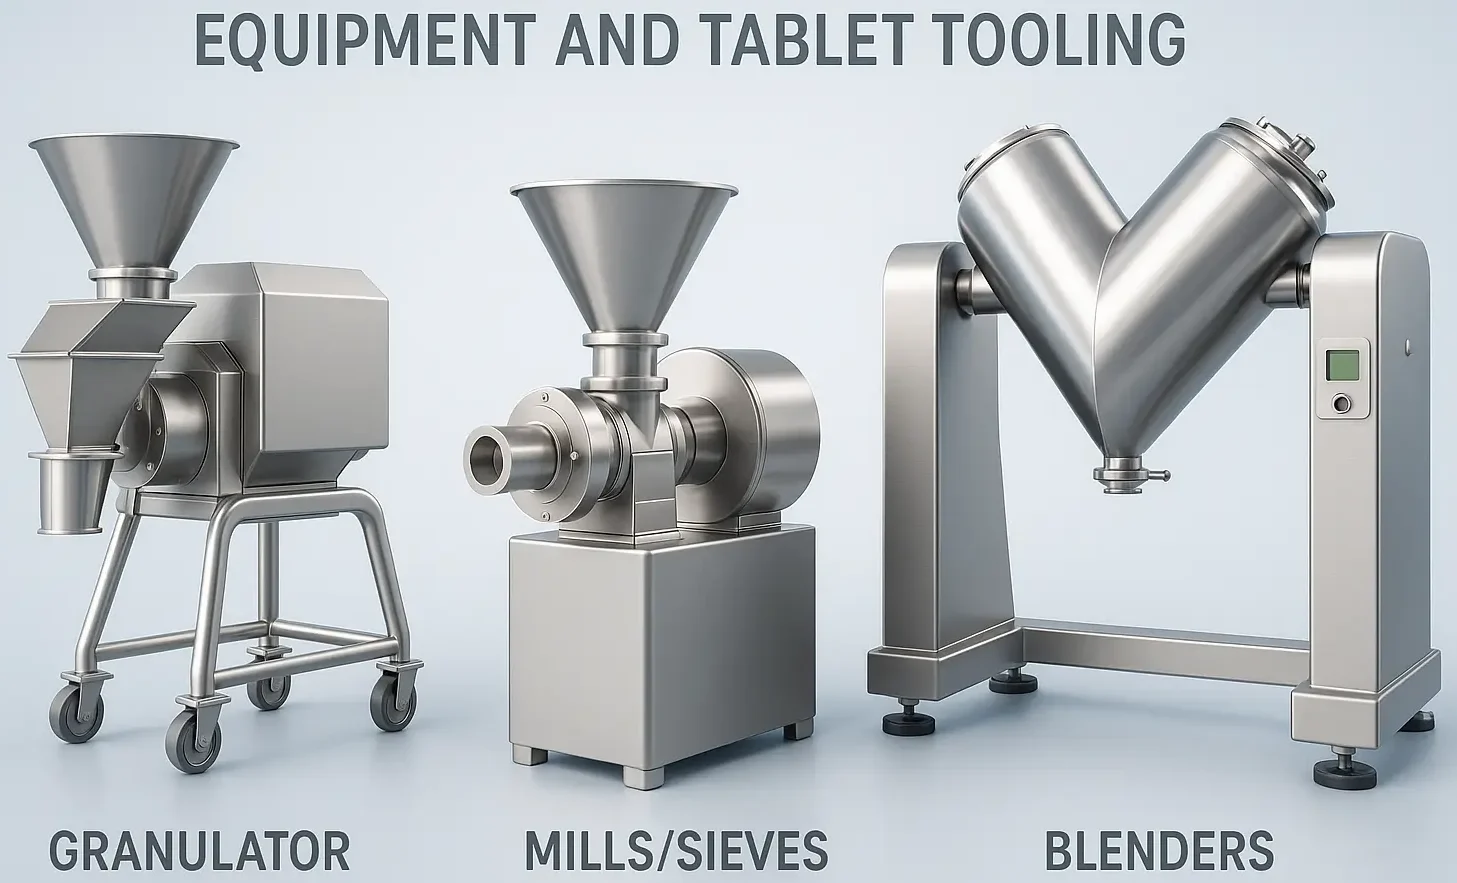
Turning a formulation into a finished tablet involves a whole bunch of distinct ...
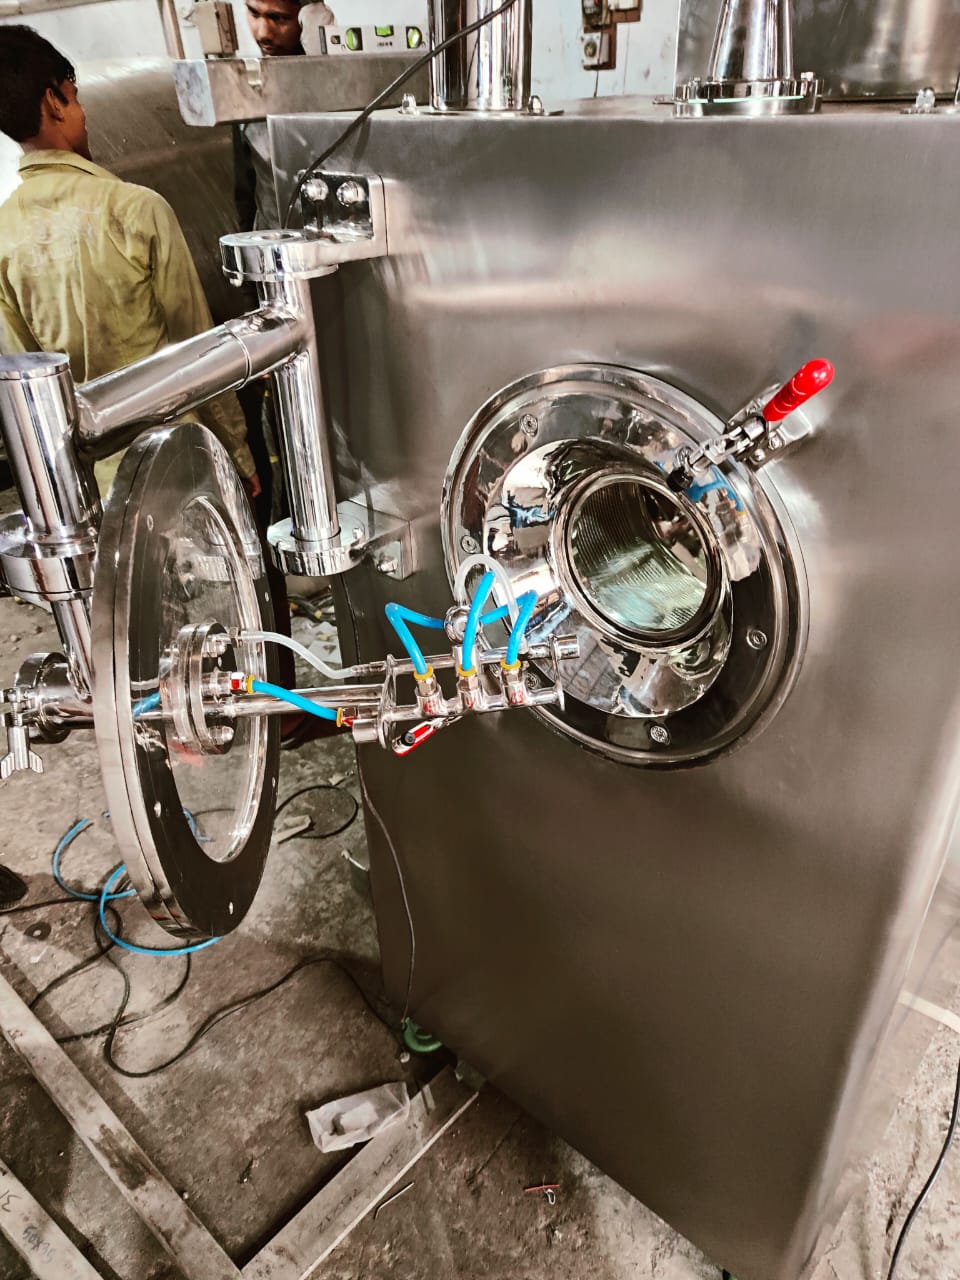
Since 2005, Pharmachem Cosmetics Industries is based in Mumbai, and has been ope...
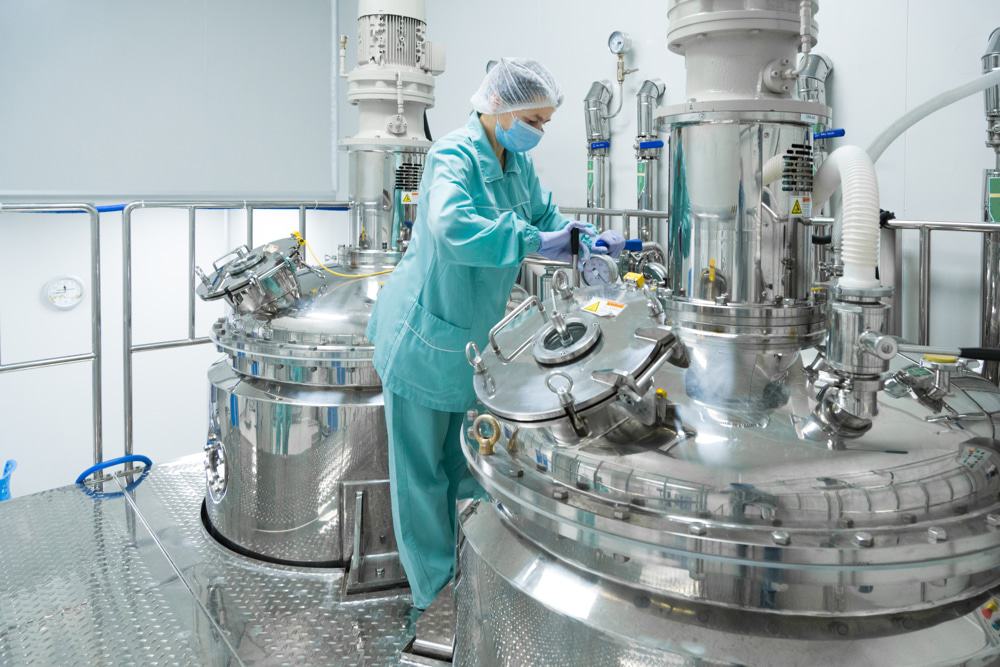
Pharmaceutical production rarely comes down to just one machine, it is usually a...
Moving heat efficiently between two fluids, without letting them mingle, sounds ...
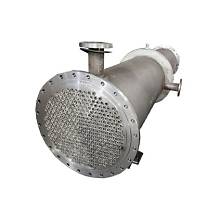
Working since 2005, Pharmachem Cosmetics Industries, headquartered in Mumbai, de...
Cream formulations live or die on emulsion stability, get the oil phase and the ...
PharmaChem Cosmetics Industries is a trusted manufacturer of GMP-compliant process equipment and complete manufacturing plants for the pharmaceutical, cosmetic, chemical, herbal, nutraceutical, and food industries. With a focus on innovation, precision engineering, and uncompromising quality, we deliver reliable stainless steel processing solutions designed to maximize productivity, efficiency, and long-term performance.
